A professional grain processing enterprise in Denmark plans to upgrade its existing rice processing line. The company aims to optimize material conveying links, upgrade food-grade conveying equipment, and meet local food safety production standards while expanding daily rice output.
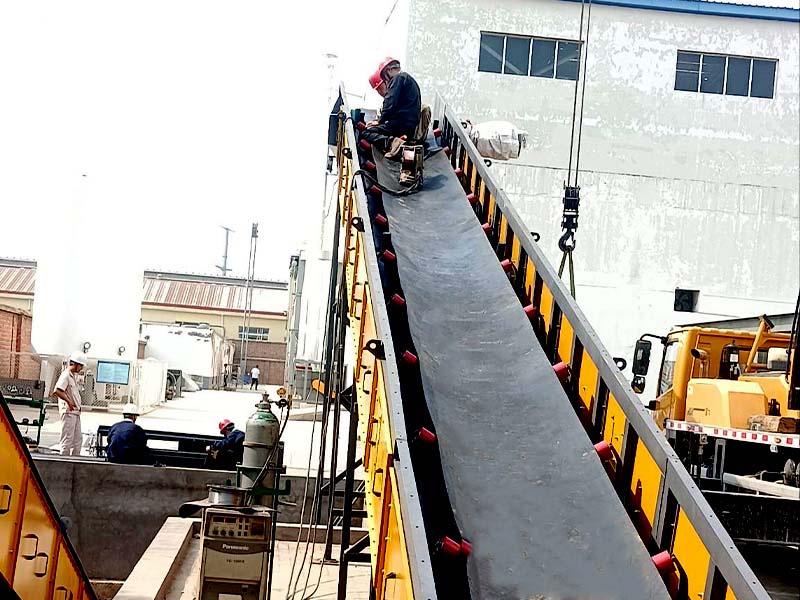
The original open-type belt conveyor has obvious drawbacks for rice processing. Open structure brings dust pollution and grain impurity contamination. Hard roller contact causes high rice broken rate during conveying. It cannot keep stable feeding speed, hindering continuous running of sorting and packaging procedures. The old equipment fails to balance production efficiency and grain integrity.
The Danish company ordered one food-grade fully enclosed belt conveyor from Yingda for full-line replacement. Our team finishes assembly, food-grade testing and factory inspection on June 12. We pack the machine with grain-dedicated protective materials and arrange direct shipment to Denmark. The conveyor will arrive at the plant site at the end of June and connect to the whole rice production line officially.
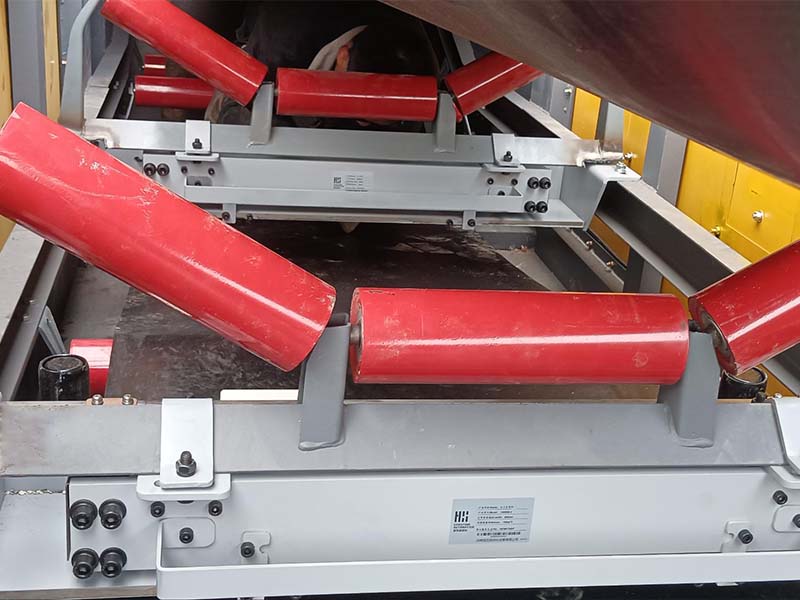
This fully enclosed belt conveyor makes up for all flaws of open conveying equipment. Its closed casing blocks dust and foreign impurities to guarantee rice food safety. It adopts soft contact conveying design to greatly cut rice broken rate. It maintains steady uniform feeding to match upstream and downstream processing equipment. The machine simplifies daily cleaning work, boosts overall line running efficiency, raises finished rice yield, and helps the enterprise gain better market competitiveness.